Metal fabrication machinery, tooling, parts & service in NY, PA, NJ, DE, MD and WV
Top 10 Types of PVC Shoe Moulds for Global Buyers?
Choosing the right Pvc Shoe Mould can determine product quality, production speed, and long-term factory costs. Global buyers must look beyond attractive prices and examine each mould’s design, material, cavity structure, and maintenance needs. A mould that performs well during a sample run may behave differently under continuous production. Small details matter. Cooling channels, venting, alignment, and surface texture can affect every pair leaving the line.
This guide reviews ten common types used for different footwear applications, including PVC injection moulds, outsole moulds, sandal moulds, boot moulds, and customized upper moulds. Each type serves a different purpose. Some support lightweight casual shoes, while others handle dense soles or demanding outdoor designs. Experienced buyers should compare steel grade, mould lifespan, replacement-part availability, and compatibility with existing machines. Supplier communication also deserves attention. Clear drawings, accurate measurements, and realistic tolerances prevent expensive revisions later.
The best choice depends on more than product appearance. It also reflects order volume, target markets, climate, packaging, and after-sales support. No single mould fits every factory. That point is easy to overlook. Even experienced teams can underestimate trial adjustments, especially when switching materials or shoe sizes. Buyers should request test samples, inspect finished edges, and record cycle times before approving mass production. This practical approach creates a more reliable purchasing decision and helps reduce waste, delays, and quality complaints across international supply chains.
PVC Shoe Mould Fundamentals: 1.30–1.45 g/cm³ Density and ISO 20344 Fit Tests
PVC shoe mould selection starts with material control, not appearance. A practical density range is 1.30–1.45 g/cm³, measured from production samples. Density affects weight, stiffness, cushioning, and mould filling behavior. It should be checked with a calibrated balance and a recorded test temperature.
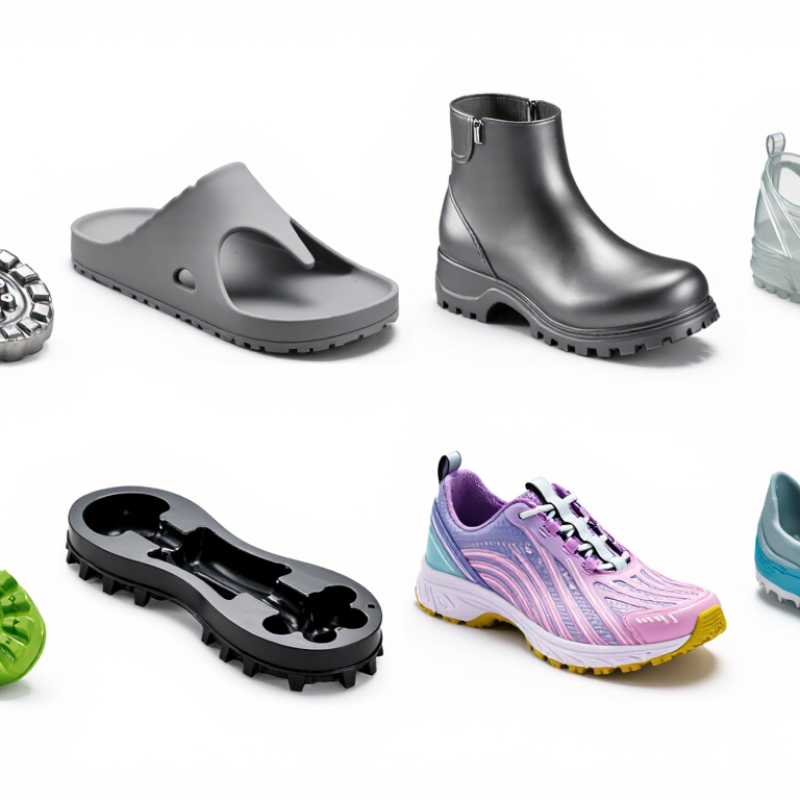
For global buyers, common options include outsole, slipper, sandal, clog, rain boot, safety boot, injection, compression, two-color, and interchangeable moulds. Each type needs suitable gates, vents, cooling channels, and shrinkage allowances. A factory trial should inspect heel seating, toe clearance, surface marks, and edge flashing. Fit-related checks should follow ISO 20344 procedures where applicable, including size consistency and internal dimensions. A shoe that looks correct may still press the toes.
Measure both left and right cavities. Small differences become uncomfortable during long wear. Density alone cannot prove quality. PVC hardness, rebound, flex resistance, and bonding also need review. I have seen attractive samples fail after repeated bending because cooling was uneven. That mistake is easy to miss. Buyers should request dimensional records, material data, and trial photos before approving tooling. Some mould designs reduce changeover time, but they may complicate cleaning and repair. A realistic evaluation includes production speed, maintenance access, expected service life, and the cost of rejected pairs. Specification sheets help, yet physical fitting remains essential. Shapes vary between users.
Top 10 Types of PVC Shoe Moulds for Global Buyers? - PVC Shoe Mould Fundamentals: 1.30–1.45 g/cm³ Density and ISO 20344 Fit Tests
| No. | PVC Shoe Mould Type | Typical Footwear Application | Mould Structure and Process | Typical Cavity Configuration | Reference PVC Density | Important Design Variables | Relevant ISO 20344 Evaluation Focus | Global Buyer Checkpoints |
|---|---|---|---|---|---|---|---|---|
| 1 | PVC Rain Boot Mould | Full-height rain boots, farm boots and general-purpose waterproof boots. | Usually a split mould or multi-part mould for injection or rotational PVC processing, with a shaped shaft and reinforced sole area. | Single cavity for tall boots; paired cavities may be used when the left and right moulds are mirrored. | 1.30–1.45 g/cm³ | Boot shaft height, ankle transition, heel counter, wall thickness, draft angle, demoulding access and upper-to-sole detailing. | Dimensional and size assessment, whole-footwear performance checks, flexing and leakage-related evaluation where applicable to the finished footwear design. | Confirm size grading, shaft circumference, wall-thickness consistency, water-tightness process and compatibility with the intended PVC compound. |
| 2 | PVC Safety Wellington Mould | Industrial safety wellingtons requiring a defined toe area and compatibility with a protective toe cap. | Heavy-duty injection mould with dedicated internal clearance for the toe-cap system and reinforced outsole geometry. | Commonly one cavity per mould set; production tooling can use multiple cavities depending on machine capacity. | 1.30–1.45 g/cm³ | Toe-cap clearance, internal volume, heel retention, outsole tread depth, instep height and demoulding around the toe box. | Footwear sizing, impact and compression testing of the completed safety footwear are normally assessed under the applicable safety-footwear standard using ISO 20344 test methods. | Validate the exact toe-cap specification, internal fit, test sample construction, outsole slip strategy and size range before final tool release. |
| 3 | PVC Chelsea Boot Mould | Short ankle boots with elastic side panels or moulded elastic-look side details. | Compact injection mould with a shaped ankle opening and side-panel relief; may include replaceable inserts for decorative details. | Single or paired cavities, generally arranged to reduce material waste and simplify parting-line finishing. | 1.30–1.45 g/cm³ | Ankle opening, instep height, pull-tab clearance, side-panel texture, heel angle and toe spring. | Size and fit verification on the finished last, plus applicable flexing, abrasion, outsole and whole-footwear checks. | Check opening recovery, ease of donning, heel hold, decorative insert life, flash location and consistency across graded sizes. |
| 4 | PVC Garden Clog Mould | Slip-on garden clogs, utility clogs and lightweight waterproof leisure footwear. | Open-top injection mould with a broad upper, integrated outsole and optional movable heel strap detail. | Two-cavity or four-cavity configurations are common for compact styles, subject to machine tonnage and cycle requirements. | 1.30–1.45 g/cm³ | Foot opening, toe-box volume, heel strap pivot, drainage considerations, tread layout and ease of ejection. | Fit and sizing review, sole flexing, slip-resistance assessment where required, abrasion and whole-footwear durability checks. | Review foot-entry comfort, strap hinge strength, flash control around the opening, mould balance and cycle-time assumptions. |
| 5 | PVC Fisherman Sandal Mould | Closed-toe or partially enclosed waterproof sandals with multiple upper straps. | Detailed injection mould with narrow strap passages, enclosed toe geometry and multiple texture or ventilation features. | Usually one cavity per size; multi-cavity tooling requires careful filling balance across thin strap sections. | 1.30–1.45 g/cm³ | Strap thickness, junction radii, toe protection, foot opening, ventilation details, gate location and weld-line control. | Dimensional fit, flexing, attachment or component integrity, abrasion and general whole-footwear performance checks. | Inspect thin-section filling, strap tear resistance, parting-line placement, foot-contact comfort and cleaning requirements. |
| 6 | PVC Slide Sandal Mould | One-piece slip-on slides for poolside, hospitality, casual and utility use. | Low-profile injection mould with an integrated sole and a broad upper strap; texture inserts can be added to the footbed. | Two-cavity or four-cavity layouts are practical for simple symmetrical styles. | 1.30–1.45 g/cm³ | Strap-to-foot clearance, footbed contour, toe-bar position, tread pattern, shrinkage allowance and gate balance. | Size verification, sole flexing, abrasion, slip-resistance testing where specified and assessment of finished footwear construction. | Confirm actual footbed length and width, strap comfort, surface texture, ejection marks, shrinkage control and size grading accuracy. |
| 7 | PVC Flip-Flop Mould | Simple thong sandals for beach, shower, hospitality and promotional applications. | Flat or contoured mould for a one-piece sole and strap system, or a sole mould designed for later strap insertion. | Multiple cavities are often suitable because the product is compact and has relatively simple geometry. | 1.30–1.45 g/cm³ | Toe-post hole geometry, strap-retention area, sole thickness, tread depth, footbed contour and cooling balance. | Dimensional and fit checks, flexing, abrasion and slip-related evaluation where the product specification requires them. | Test strap pull-out strength, toe-post comfort, sole flatness, cavity-to-cavity weight variation and resistance to warpage. |
| 8 | PVC House Slipper Mould | Closed-toe indoor slippers, bathroom slippers and washable utility footwear. | Injection mould with a soft-looking upper profile, enclosed toe box and textured or cushioned footbed features. | Single or paired cavities are common; cavity count depends on upper complexity and required surface finish. | 1.30–1.45 g/cm³ | Toe-box height, opening shape, heel cup, footbed texture, thermal comfort considerations and soft-edge radii. | Fit and size assessment, flexing, abrasion, sole performance and inspection of finished footwear for dimensional consistency. | Check entry opening, heel security, footbed comfort, surface cleanliness, texture release and tolerance control after cooling. |
| 9 | PVC Work Clog Mould | Slip-on work clogs for cleaning, food-service and light industrial environments. | Reinforced injection mould with a closed or semi-closed upper, raised heel area and pronounced outsole tread. | Typically one or two cavities, allowing greater control over thick sections and dense tread geometry. | 1.30–1.45 g/cm³ | Heel counter, instep opening, tread depth, sidewall reinforcement, drainage geometry and material distribution. | Whole-footwear flexing, abrasion, slip-resistance evaluation where specified, dimensional fit and relevant component-performance checks. | Confirm slip-test requirements for the target market, tread cleanability, heel retention, weight balance and resistance to repeated flexing. |
| 10 | PVC Fashion Ankle Boot Mould | Decorative ankle boots with sculpted heels, embossed surfaces or fashion-focused outsole profiles. | Precision injection mould with interchangeable cosmetic inserts or engraved surfaces for patterns, logos or textures without relying on brand-specific data. | Usually single-cavity tooling to protect cosmetic quality and maintain accurate alignment of decorative surfaces. | 1.30–1.45 g/cm³ | Cosmetic surface quality, heel geometry, ankle opening, toe shape, texture depth, parting-line visibility and shrinkage compensation. | Fit and size verification, flexing, abrasion, outsole performance and inspection of the finished footwear against the approved sample. | Approve a textured trial sample, verify surface release, inspect flash on visible areas, confirm heel stability and document colour or finish tolerances. |
Technical note: The 1.30–1.45 g/cm³ range is a practical reference range for many rigid or semi-flexible PVC footwear compounds; the final density depends on resin, plasticizer, filler, pigment, blowing agent and processing conditions. ISO 20344 provides footwear test methods and does not by itself define one universal fit-test pass level. Final compliance should be confirmed against the applicable product standard, market regulation and approved footwear specification.